United Chemicals Job Offers - Join Our Global Team of Chemistry Experts
Discover exciting career opportunities at United Chemical. Join our global team and shape the future of the chemical industry with innovation and expertise. Apply today!

Discover exciting career opportunities at United Chemical. Join our global team and shape the future of the chemical industry with innovation and expertise. Apply today!
Empowering African Gold Miners: Premium Extraction Chemicals Now Available in Local Spot Stock
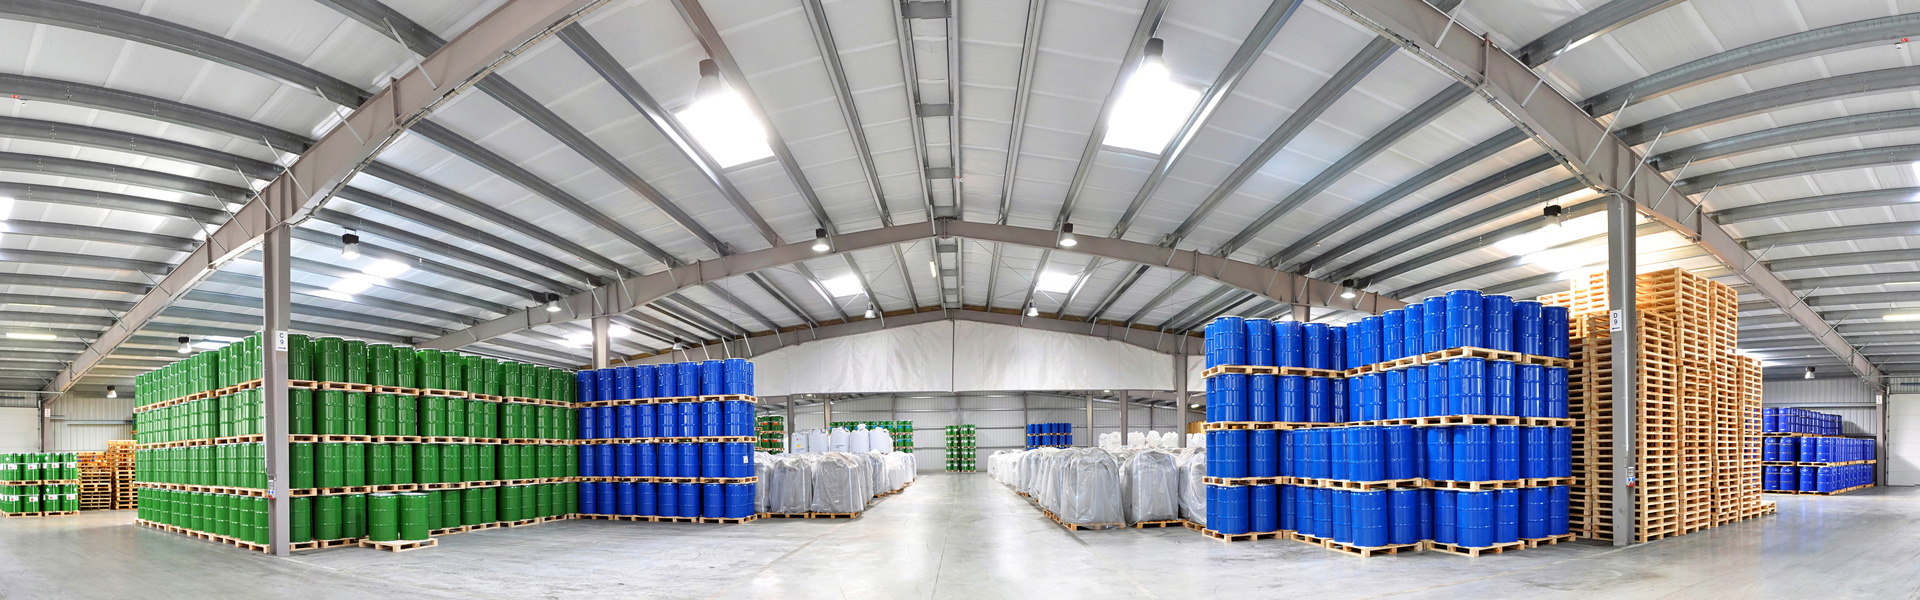
Time is gold in the mining industry. Waiting 45 to 60 days for international sea freight can severely impact your production schedule and tie up crucial cash flow. To bridge this gap, United Chemical has officially established two strategic front-warehouses in East and Southern Africa, bringing our world-class reagents directly to your doorstep.

Eliminate the 2-month sea freight waiting period. Keep your CIL tanks running without interruption.
No need to lock up capital in Full Container Loads (FCL). Our local warehouses support a minimum order quantity (MOQ) of just 1 Metric Ton , available in both 50kg steel drums and 1-ton / 1.1-ton wooden boxes , perfectly matching your production scale.
Buy directly from the manufacturer's local stock. No middlemen, no compromised packaging.
* Important Notice: All purchasers must possess and provide valid legal permits, licenses, and procedures to purchase, transport, and use these mineral extraction chemicals in strict compliance with local laws and regulations.
Our facilities are strategically located along major logistics corridors to ensure rapid deployment to active mining regions, providing seamless overland logistics even to landlocked nations like Zimbabwe and Zambia.
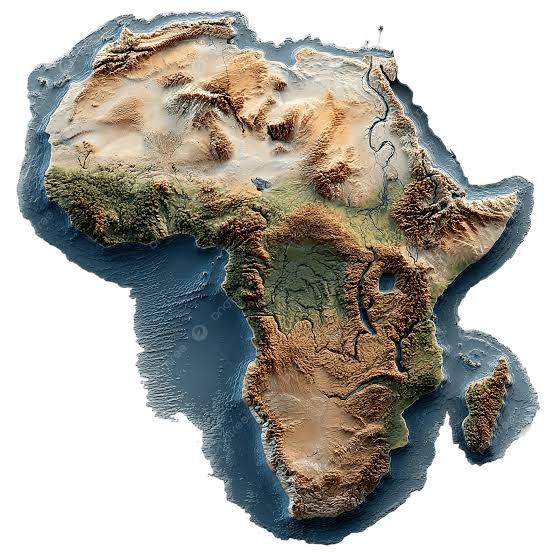
Location: Chalinze-Segera Highway (A14), Lugoba Area..
Coverage & Logistics: Provides rapid response to major gold belts across Tanzania (such as Geita and Manyara) and acts as a central distribution hub for neighboring East African mining sectors.
Location: EN6 Highway (Beira Corridor), Warehouse Zone, Beira, Sofala Province.
Coverage & Logistics: Serves as the ultimate deep-water gateway for Mozambique. Crucially, it provides highly efficient, seamless overland trucking logistics directly into the Manicaland gold belt in Zimbabwe and active mining sectors in Zambia.
We stock the industry's most reliable and strictly tested extraction reagents, tailored for maximizing recovery rates in African geology:
Positioning: The performance and purity benchmark for traditional cyanidation in medium-to-large scale gold mining operations.
Core Selling Points:≥98.3% High Purity | Low Reagent Single-Consumption | Full International Hazmat Compliance
AuCyan™ represents United Chemical's pursuit of perfection in foundational mineral processing chemicals. As the most efficient traditional leaching reagent, we adhere to strict industrial standards to ensure batch-to-batch purity and stability, providing essential momentum for gold mining facilities worldwide. When paired with high-quality activated carbon, it ensures the most efficient dissolution and capture of gold ions.
≥98.3% High-Purity Standard: Purity levels far exceeding industry standards guarantee maximum active free cyanide ions (CN−) during cyanidation. This drastically accelerates gold/silver dissolution kinetics and maximizes overall leaching efficiency.
Cost-Effective Consumption Control: Ultra-low impurity levels minimize unwanted side-reactions with accompanying minerals (such as copper, iron, and sulfur) in the leaching slurry, significantly lowering reagent consumption per ton of ore processed.
Global-Grade Export Compliance & Delivery: As a regulated dangerous good, supply chain expertise is paramount. United Chemical holds robust UN-certified packaging solutions (steel drums, wooden boxes, Isotanks) and international export qualifications, guaranteeing smooth, safe, and compliant delivery to over 90 gold-producing nations.
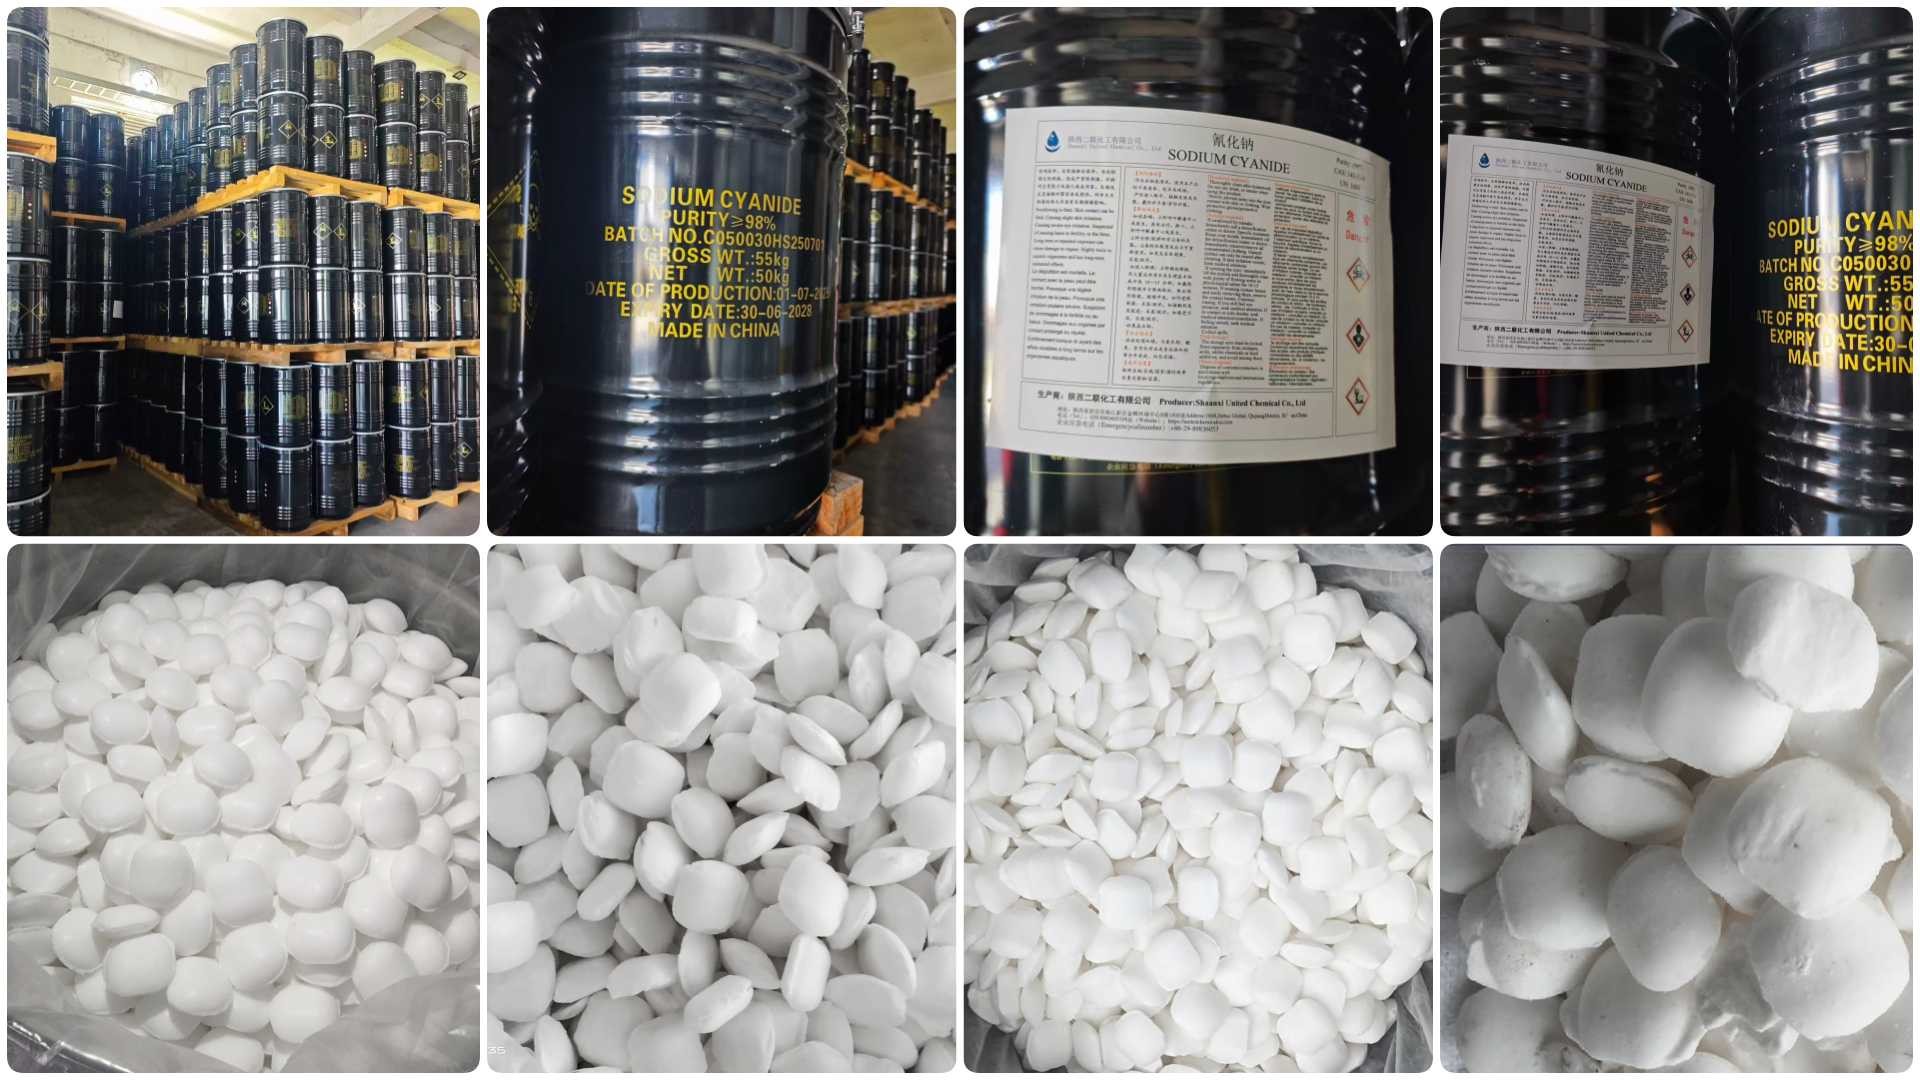
Surpassing industry benchmarks, our latest production batches consistently achieve "Superior Quality" grades. Below is the certified performance data (Ref: Batch C050030HS251101).
| Testing Items | Standard (GB/T 19306-2003) | AuCyan™ (Typical) | Operational Impact |
|---|---|---|---|
| Sodium Cyanide (NaCN) | ≥ 98.0% | 98.3% | Maximum gold dissolution kinetics and recovery rates. |
| Sodium Hydroxide (NaOH) | ≤ 0.5% | 0.13% | Superior pH stability; prevents premature hydrolysis. |
| Sodium Carbonate (Na₂CO₃) | ≤ 0.5% | 0.18% | Minimized impurity interference in the leaching solution. |
| Moisture (H₂O) | ≤ 0.9% | 0.3% | Enhanced solid stability during long-term storage and sea transit. |
| Insoluble Substances | ≤ 0.05% | 0.02% | Anti-clogging formula; protects critical pumps and nozzles. |
Positioning: Custom-engineered high-strength, high-adsorption coconut carbon tailored for CIP / CIL / CIC gold recovery circuits.
Core Selling Points: Ultra-High Hardness (≥99%) | Rapid Gold-Complex Adsorption Kinetics | High Reactivation Yield
In CIP/CIL processes, activated carbon quality directly determines final gold output. AuCarb™ is custom-developed for harsh agitation environments, refined from top-tier Sri Lankan and Southeast Asian coconut shells through high-temperature activation and polishing treatments. It is designed to act as the ultimate gold capture matrix, perfectly complimenting our leaching agents.
Ultra-High Hardness & Attrition Resistance (Minimal Gold Loss): Mine operators fear carbon attrition in leach tanks leading to gold fines loss. AuCarb™ undergoes special hardening treatment to achieve a hardness rating above ≥99%, completely eliminating costly "gold-bearing carbon" breakdown.
Rapid & High-Capacity Pore Architecture (High Adsorption Kinetics): Gold-cyanide complexes are larger molecular structures. AuCarb™ features a precisely controlled ratio of micro-pores to meso-pores, ensuring rapid entry and firm entrapment of [Au(CN)₂]⁻ complexes with loading capacity far surpassing standard activated carbons.
Extended Service Life & High Reactivation Yield: Following desorption-electrowinning, AuCarb™ recovers over 95% of its original activity after thermal reactivation. It can be recycled through multiple cycles, significantly lowering carbon replacement costs per ton of gold produced.

To facilitate a more intuitive selection process tailored to your specific metallurgy circuit, we have summarized the core technical parameters of our four flagship AuCarb™ variants.
| Core Testing Parameter | AuCarb™ BC1100 | AuCarb™ AC50 | AuCarb™ AC55 | AuCarb™ AC60 |
|---|---|---|---|---|
| Market Benchmarking Positioning | Conventional Heap Leach | Comparable: Jacobi G208AS | Comparable: Jacobi G209AS | Advanced: Jacobi G210AS |
| Apparent Density | 0.40 - 0.50 g/ml | 0.48 - 0.55 g/ml | 0.45 - 0.55 g/ml | 0.45 - 0.55 g/ml |
| Ball-pan Hardness | ≥ 98.5% | ≥ 99% | ≥ 99% | ≥ 99% |
| Platelet Content | ≤ 5% | ≤ 5% | ≤ 5% | ≤ 5% |
| Attrition | ≤ 2% | ≤ 1.5% | ≤ 2% | ≤ 2% |
| Total Ash Content | ≤ 5% | ≤ 3% | ≤ 3% | ≤ 3% |
| Moisture | ≤ 10% | ≤ 5% | ≤ 5% | ≤ 5% |
| Adsorption Capacity (K Value) | / | ≥ 26 Kg/t | ≥ 28 Kg/t | ≥ 30 Kg/t |
| Adsorption Rate (R Value) | / | ≥ 50% | ≥ 55% | ≥ 60% |
| Iodine Number | ≥ 1100 mg/g | / | / | / |
| Butane Activity | / | ≥ 19.5% | ≥ 21% | ≥ 23% |
| CTC (Carbon Tetrachloride Activity) | / | ≥ 50% | ≥ 55% | / |
Applicable Metallurgy Processes:Carbon-in-Pulp (CIP), Carbon-in-Leach (CIL), Carbon-in-Column (CIC), Heap Leaching, VAT Leaching.
Positioning: A non-toxic leaching agent balancing high recovery yields with strict HSE environmental compliance.
Core Selling Points: General Cargo Export (Non-Hazardous) | Zero Equipment Modification | Superior Yield on Refractory Ores
Faced with increasingly stringent global environmental regulations (HSE), many gold mines face restrictions or bans on cyanide usage. AuLeach™ Eco-Friendly Gold Leaching Agent offers the perfect 100% green replacement for sodium cyanide, aligning "green mining" with high financial returns.
Seamless Direct Drop-in Replacement: Transitioning to AuLeach™ requires zero modification to existing cyanidation equipment (such as Heap Leaching or CIL circuits). It can be directly substituted for sodium cyanide at 1:1 or recommended ratios to immediately start production.
Non-Toxic Certification & Streamlined Approval (HSE Compliance): Officially certified as a general chemical (Non-Hazmat). This dramatically reduces ocean freight, land logistics, and insurance costs while eliminating tedious toxic chemical permit approvals, cutting mine commissioning lead times by over 50%.
Faster Kinetics & Superior Performance on Refractory Ores: When treating complex, refractory gold ores containing arsenic or sulfur, AuLeach™ exhibits superior resistance to interference and faster leaching kinetics compared to NaCN, frequently achieving a 2% to 5% increase in absolute recovery rate.
Safe Working Environment & ESG Value: Drastically reduces occupational health risks for operational personnel and minimizes environmental contamination hazards, making it the preferred reagent for modern mining companies seeking high ESG ratings.
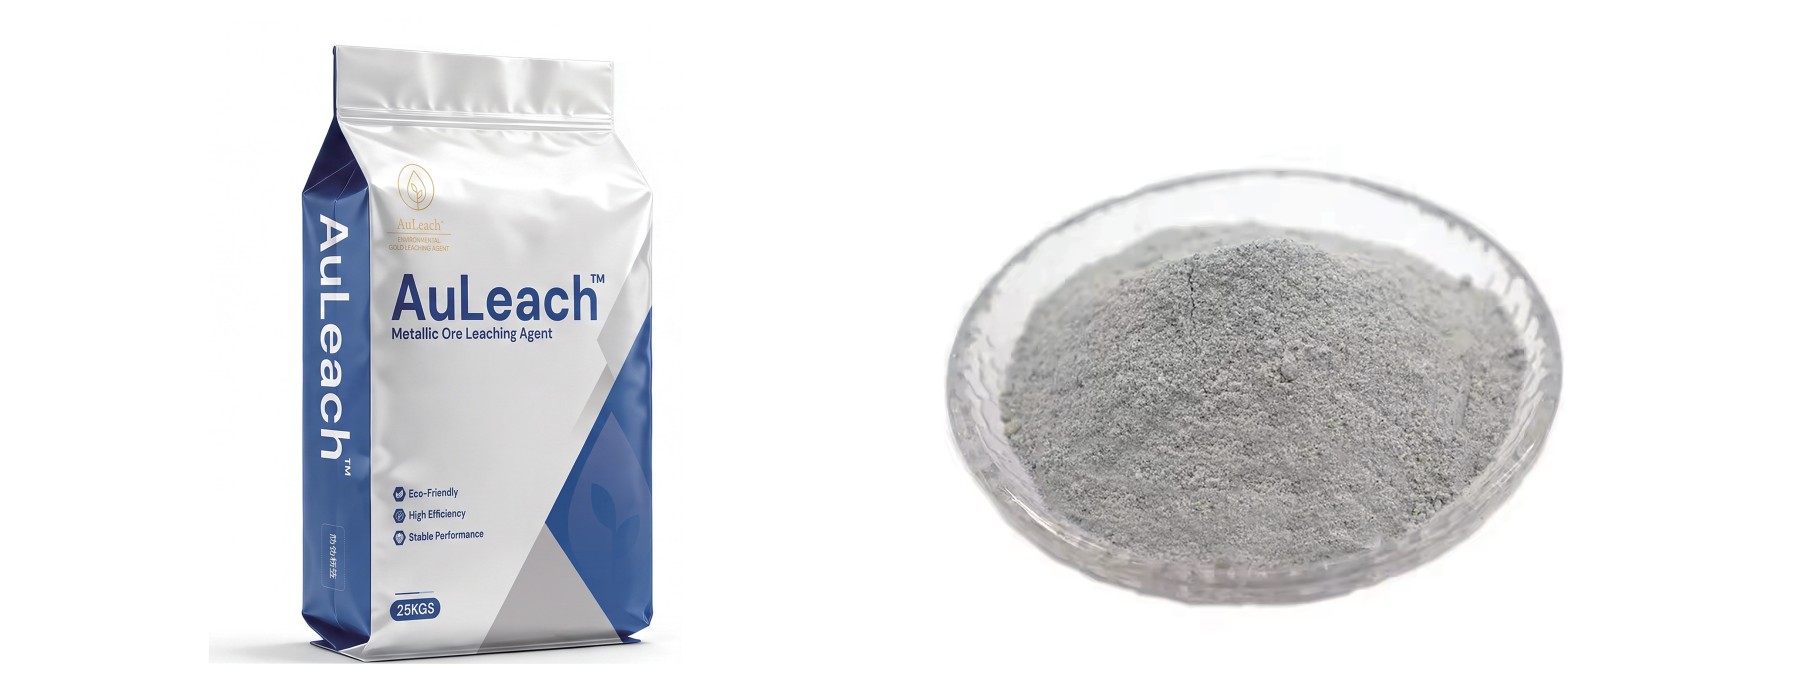
| Parameter | Units | Guaranteed Specification |
|---|---|---|
| Appearance | - | Solid Powder |
| Operational pH Range | - | 10.5 - 12 |
| Leaching Agent Concentration | % | 30 |
| Standard Packaging | Kgs | Net 25Kgs bag |
Broad Application Spectrum: Highly effective across primary ores, oxide ores, semi-oxide ores, sulfide ores, gold concentrates, and cyanide tailings in both Carbon-in-Pulp and Pool/Vat leaching circuits.
Zero Equipment CAPEX: Fully compatible with existing Chilean Heap leaching and CIL infrastructure. Requires absolutely no mechanical retrofitting.
Unrestricted Logistics: Shipped and trucked as general cargo, eliminating the exorbitant costs of hazardous goods import permits at ports like Antofagasta and specialized DG escorts across the Atacama.
Stop waiting for international shipments. Keep your processing plant operating at maximum capacity. Contact our team to check real-time inventory levels, request an immediate quote, or schedule a pickup from our Lugoba or Beira facilities.
📍 Headquarters: Jinhui Global, Qujiang District, Xi'an, Shaanxi Province, China
📱 Mobile / WhatsApp:+86 17392705576
✉️ Email:info@unitedchemicalcn.com
🌐 Website:unitedchemicalcn.com
Focusing on Gold Mining & Precious Metal Extraction Solutions.
Pioneer | Collaborate | Communicate | Dedicated | Honesty | Win-win
Explore Premium AuCyan™ Sodium Cyanide, AuCarb™ Coconut Activated Carbon, and AuLeach™ Eco-Friendly Leaching Agent.
As a premier global one-stop supplier of gold mining chemicals, United Chemical delivers an elite product line covering the complete metallurgical circuit: Leaching – Adsorption – Eco-Friendly Substitution. We empower global mining enterprises to break through extraction efficiency ceilings and maximize gold yield per ton.
Synergy Driven Performance: Whether you are utilizing the industry benchmark AuCyan™, seamlessly pairing it with our premium AuCarb™ coconut activated carbon for flawless CIP/CIL adsorption, or transitioning to green mining with AuLeach™, our integrated solutions are engineered to work in perfect harmony, minimizing reagent consumption while maximizing your gold bar output.
Positioning: The performance and purity benchmark for traditional cyanidation in medium-to-large scale gold mining operations.
Core Selling Points:≥98.3% High Purity | Low Reagent Single-Consumption | Full International Hazmat Compliance
AuCyan™ represents United Chemical's pursuit of perfection in foundational mineral processing chemicals. As the most efficient traditional leaching reagent, we adhere to strict industrial standards to ensure batch-to-batch purity and stability, providing essential momentum for gold mining facilities worldwide. When paired with high-quality activated carbon, it ensures the most efficient dissolution and capture of gold ions.
≥98.3% High-Purity Standard: Purity levels far exceeding industry standards guarantee maximum active free cyanide ions (CN−) during cyanidation. This drastically accelerates gold/silver dissolution kinetics and maximizes overall leaching efficiency.
Cost-Effective Consumption Control: Ultra-low impurity levels minimize unwanted side-reactions with accompanying minerals (such as copper, iron, and sulfur) in the leaching slurry, significantly lowering reagent consumption per ton of ore processed.
Global-Grade Export Compliance & Delivery: As a regulated dangerous good, supply chain expertise is paramount. United Chemical holds robust UN-certified packaging solutions (steel drums, wooden boxes, Isotanks) and international export qualifications, guaranteeing smooth, safe, and compliant delivery to over 90 gold-producing nations.
Surpassing industry benchmarks, our latest production batches consistently achieve "Superior Quality" grades. Below is the certified performance data (Ref: Batch C050030HS251101).
| Testing Items | Standard (GB/T 19306-2003) | AuCyan™ (Typical) | Operational Impact |
|---|---|---|---|
| Sodium Cyanide (NaCN) | ≥ 98.0% | 98.3% | Maximum gold dissolution kinetics and recovery rates. |
| Sodium Hydroxide (NaOH) | ≤ 0.5% | 0.13% | Superior pH stability; prevents premature hydrolysis. |
| Sodium Carbonate (Na₂CO₃) | ≤ 0.5% | 0.18% | Minimized impurity interference in the leaching solution. |
| Moisture (H₂O) | ≤ 0.9% | 0.3% | Enhanced solid stability during long-term storage and sea transit. |
| Insoluble Substances | ≤ 0.05% | 0.02% | Anti-clogging formula; protects critical pumps and nozzles. |
Positioning: Custom-engineered high-strength, high-adsorption coconut carbon tailored for CIP / CIL / CIC gold recovery circuits.
Core Selling Points: Ultra-High Hardness (≥99%) | Rapid Gold-Complex Adsorption Kinetics | High Reactivation Yield
In CIP/CIL processes, activated carbon quality directly determines final gold output. AuCarb™ is custom-developed for harsh agitation environments, refined from top-tier Sri Lankan and Southeast Asian coconut shells through high-temperature activation and polishing treatments. It is designed to act as the ultimate gold capture matrix, perfectly complimenting our leaching agents.
Ultra-High Hardness & Attrition Resistance (Minimal Gold Loss): Mine operators fear carbon attrition in leach tanks leading to gold fines loss. AuCarb™ undergoes special hardening treatment to achieve a hardness rating above ≥99%, completely eliminating costly "gold-bearing carbon" breakdown.
Rapid & High-Capacity Pore Architecture (High Adsorption Kinetics): Gold-cyanide complexes are larger molecular structures. AuCarb™ features a precisely controlled ratio of micro-pores to meso-pores, ensuring rapid entry and firm entrapment of [Au(CN)₂]⁻ complexes with loading capacity far surpassing standard activated carbons.
Extended Service Life & High Reactivation Yield: Following desorption-electrowinning, AuCarb™ recovers over 95% of its original activity after thermal reactivation. It can be recycled through multiple cycles, significantly lowering carbon replacement costs per ton of gold produced.
To facilitate a more intuitive selection process tailored to your specific metallurgy circuit, we have summarized the core technical parameters of our four flagship AuCarb™ variants.
| Core Testing Parameter | AuCarb™ BC1100 | AuCarb™ AC50 | AuCarb™ AC55 | AuCarb™ AC60 |
|---|---|---|---|---|
| Market Benchmarking Positioning | Conventional Heap Leach | Comparable: Jacobi G208AS | Comparable: Jacobi G209AS | Advanced: Jacobi G210AS |
| Apparent Density | 0.40 - 0.50 g/ml | 0.48 - 0.55 g/ml | 0.45 - 0.55 g/ml | 0.45 - 0.55 g/ml |
| Ball-pan Hardness | ≥ 98.5% | ≥ 99% | ≥ 99% | ≥ 99% |
| Platelet Content | ≤ 5% | ≤ 5% | ≤ 5% | ≤ 5% |
| Attrition | ≤ 2% | ≤ 1.5% | ≤ 2% | ≤ 2% |
| Total Ash Content | ≤ 5% | ≤ 3% | ≤ 3% | ≤ 3% |
| Moisture | ≤ 10% | ≤ 5% | ≤ 5% | ≤ 5% |
| Adsorption Capacity (K Value) | / | ≥ 26 Kg/t | ≥ 28 Kg/t | ≥ 30 Kg/t |
| Adsorption Rate (R Value) | / | ≥ 50% | ≥ 55% | ≥ 60% |
| Iodine Number | ≥ 1100 mg/g | / | / | / |
| Butane Activity | / | ≥ 19.5% | ≥ 21% | ≥ 23% |
| CTC (Carbon Tetrachloride Activity) | / | ≥ 50% | ≥ 55% | / |
Positioning: A non-toxic leaching agent balancing high recovery yields with strict HSE environmental compliance.
Core Selling Points: General Cargo Export (Non-Hazardous) | Zero Equipment Modification | Superior Yield on Refractory Ores
Faced with increasingly stringent global environmental regulations (HSE), many gold mines face restrictions or bans on cyanide usage. AuLeach™ Eco-Friendly Gold Leaching Agent offers the perfect 100% green replacement for sodium cyanide, aligning "green mining" with high financial returns.
Seamless Direct Drop-in Replacement: Transitioning to AuLeach™ requires zero modification to existing cyanidation equipment (such as Heap Leaching or CIL circuits). It can be directly substituted for sodium cyanide at 1:1 or recommended ratios to immediately start production.
Non-Toxic Certification & Streamlined Approval (HSE Compliance): Officially certified as a general chemical (Non-Hazmat). This dramatically reduces ocean freight, land logistics, and insurance costs while eliminating tedious toxic chemical permit approvals, cutting mine commissioning lead times by over 50%.
Faster Kinetics & Superior Performance on Refractory Ores: When treating complex, refractory gold ores containing arsenic or sulfur, AuLeach™ exhibits superior resistance to interference and faster leaching kinetics compared to NaCN, frequently achieving a 2% to 5% increase in absolute recovery rate.
Safe Working Environment & ESG Value: Drastically reduces occupational health risks for operational personnel and minimizes environmental contamination hazards, making it the preferred reagent for modern mining companies seeking high ESG ratings.
| Parameter | Units | Guaranteed Specification |
|---|---|---|
| Appearance | - | Solid Powder |
| Operational pH Range | - | 10.5 - 12 |
| Leaching Agent Concentration | % | 30 |
| Standard Packaging | Kgs | Net 25Kgs bag |
Broad Application Spectrum: Highly effective across primary ores, oxide ores, semi-oxide ores, sulfide ores, gold concentrates, and cyanide tailings in both Carbon-in-Pulp and Pool/Vat leaching circuits.
Zero Equipment CAPEX: Fully compatible with existing Chilean Heap leaching and CIL infrastructure. Requires absolutely no mechanical retrofitting.
Unrestricted Logistics: Shipped and trucked as general cargo, eliminating the exorbitant costs of hazardous goods import permits at ports like Antofagasta and specialized DG escorts across the Atacama.
From high-efficiency leaching (AuCyan™ / AuLeach™) to precision adsorption enrichment (AuCarb™), United Chemical provides an industry-leading "Golden Triangle" solution matrix. We are more than chemical manufacturers—we are technical experts committed to maximizing the economic yield of every ton of your ore.
≥98.3% High-purity NaCN. The industry standard for maximum leaching kinetics and low reagent consumption.
High active CN− concentration
UN-certified export compliance
Ideal for CIL, CIP & Heap Leaching
Premium coconut shell activated carbon with ≥99% hardness to minimize gold loss during CIL/CIP agitation.
Ultra-high attrition resistance
Fast gold adsorption kinetics
>95% Activity recovery after desorption
Non-toxic 100% cyanide alternative (GDA). Seamless drop-in replacement with fast customs clearance.
Non-hazardous logistics & easy clearance
Zero equipment modification needed
Higher recovery on refractory ores
Explore our comprehensive technical, logistical, and metallurgical database. From managing complex high-copper ores to navigating global hazardous logistics, find expert answers covering AuCyan™, AuCarb™, and AuLeach™.
The Golden Triangle represents United Chemical's proprietary matrix of three essential mining reagents: AuCyan™ (high-purity sodium cyanide for traditional leaching), AuCarb™ (ultra-hard activated carbon for capturing dissolved gold), and AuLeach™ (an eco-friendly, non-hazardous leaching alternative). Together, they provide a 360-degree solution for any geological or regulatory challenge globally.
Consolidating your supply chain with our Golden Triangle ensures perfect chemical compatibility in your CIL/CIP circuits. Furthermore, bundling these reagents under a single factory-direct supplier optimizes maritime container space, reduces aggregate freight costs, and simplifies customs clearance.
To ensure factory-direct pricing, protect packaging integrity, and optimize maritime freight, our strict Minimum Order Quantity (MOQ) across all products is 1x20' FCL (Full Container Load).
Yes, we provide complimentary laboratory samples strictly for AuCarb™ Activated Carbon and AuLeach™ Eco-Friendly Agent. Due to strict international hazardous materials regulations, we cannot dispatch small samples of AuCyan™ (Sodium Cyanide) via express air freight.
United Chemical proudly exports to over 77 countries, dominating major mining hubs including Latin America (Mexico, Peru, Chile), Africa (Ghana, Mali, Tanzania), Southeast Asia (Indonesia, Philippines), and Central Asia.
All our reagents are engineered as "drop-in" solutions. Whether you use AuCyan™ or transition to the eco-friendly AuLeach™, you require zero equipment modification to your existing Heap leach pads or CIL/CIP tanks, eliminating heavy capital expenditures (CAPEX).
Yes, our technical engineering team analyzes your specific ore characteristics (e.g., silver ratio, copper content, clay viscosity) and recommends the precise AuCarb™ mesh size and leaching reagent concentration to optimize your recovery curve.
Yes, for qualified international distributors ordering consistently in bulk, we offer customized OEM packaging solutions, particularly for AuCarb™ and AuLeach™, ensuring your brand maintains a strong regional presence.
For standard 1x20' FCL orders, production and custom packaging are typically completed within 10 to 14 business days, ready for immediate loading onto vessels at major Chinese maritime ports.
Absolutely. AuCyan™ complies strictly with GB/T 19306 standards, AuCarb™ is tested under ASTM and AARL methodologies, and AuLeach™ is certified by global testing agencies (like SGS) as a non-hazardous substance.
Yes, for mid-to-large scale mining operations, we establish long-term supply agreements. This stabilizes your OPEX against global chemical market fluctuations and guarantees priority production scheduling.
Standard industrial cyanide often tests at 97%. AuCyan™ guarantees ≥98.3% purity. This higher concentration ensures a massive surplus of free CN⁻ ions, which rapidly penetrates complex ore matrices, slashing required leaching times and maximizing yield.
AuCyan™ maintains sodium hydroxide (NaOH) levels around 0.13%. This provides excellent pH buffering to prevent premature hydrolysis (off-gassing) without causing severe calcium scaling in your Heap Leach drip emitters and pipelines.
AuCyan™ is manufactured as solid white briquettes (tablets). This shape minimizes dangerous dust generation during handling, dissolves rapidly in mixing tanks, and is highly stable during long ocean transits.
Copper aggressively consumes cyanide. AuCyan™’s ultra-high purity ensures that even after base metals (like copper or zinc) consume their stoichiometric share of CN⁻ ions, sufficient active cyanide remains to rapidly dissolve the target gold particles.
AuCyan™ features an ultra-low moisture content of ≤0.3%. High moisture leads to chemical degradation and hazardous ammonia gas buildup inside the drum. Our dry formulation guarantees long-term stability in tropical climates.
No. With insoluble substances strictly controlled at ≤0.02%, AuCyan™ dissolves cleanly into a clear liquor, preventing sludge buildup in your tanks and protecting expensive slurry pumps from premature wear.
It is exported in UN-certified 50kg hermetically sealed steel drums or 1,000kg reinforced wooden boxes. Both options feature a heavy-duty, heat-sealed Polyethylene (PE) inner liner to completely block atmospheric moisture.
AuCyan™ Sodium Cyanide is strictly classified under UN 1689, designated as a Class 6.1 Toxic Substance (Dangerous Goods) under international maritime law.
While it varies by ore type, operators typically mix the solid briquettes with process water to create a high-strength stock solution (typically 10% to 20% NaCN by weight) before dosing it into the leaching circuit to maintain optimal PPM levels.
Absolutely. Silver extraction requires significantly higher cyanide concentrations than gold. AuCyan™’s extreme 98.3% purity is highly sought after by epithermal silver-gold operations (such as in Mexico) to satisfy massive reagent consumption.
When kept in its original, unbroken, UN-certified packaging within a dry, well-ventilated warehouse out of direct sunlight, AuCyan™ maintains optimal chemical stability for up to 12 to 24 months.
Coconut shell carbon possesses a naturally dense, micro-porous structure perfectly sized for the [Au(CN)₂]⁻ complex. It offers significantly higher mechanical hardness and a much lower ash content compared to coal or wood-based carbons, minimizing fine gold losses.
In CIL/CIP tanks, the mechanical agitation is violent. If carbon is soft, it shatters into fine dust that carries adsorbed gold out into the tailings dam. AuCarb™’s ≥99% hardness ensures massive structural integrity, reducing attrition to near zero.
6x12 mesh particles are larger and coarser, commonly used in Heap Leaching (CIC) to handle high flow rates without clogging. 8x16 mesh particles are finer, offering higher surface area for faster adsorption kinetics in CIL/CIP tank agitation.
The K-Value (Adsorption Capacity) measures the total amount of gold the carbon can hold at equilibrium (e.g., ≥30 Kg/t). The R-Value (Adsorption Rate) measures how fast the carbon loads gold. AuCarb™ AC60 excels in both, boasting R-Values ≥60%.
Platelets are flat, poorly shaped carbon granules that can easily slip through inter-tank screens, carrying gold to the tailings. AuCarb™ guarantees a platelet content of ≤5%, ensuring precision screening and maximum gold retention.
Yes, AuCarb™ features a pristine pore network that releases gold complexes rapidly under high-temperature/high-pressure elution conditions (both Zadra and AARL), resulting in a highly concentrated pregnant solution for electrowinning.
Absolutely. After acid washing and elution, AuCarb™ can be passed through a rotary kiln at ~700°C. Its high density allows it to recover over 95% of its original activity over multiple cycles, significantly reducing OPEX.
Preg-robbing ores contain natural carbon that prematurely steals dissolved gold. To combat this, you need an activated carbon with colossal kinetic speed. AuCarb™’s extreme CTC and Iodine numbers allow it to instantly out-compete native carbon for gold complexes.
High ash content indicates inorganic impurities that can blind the carbon's pores and interfere with gold loading. AuCarb™’s ultra-low ash (≤3%) ensures maximum pore availability and cleaner elution profiles.
While all carbon can adsorb organic matter (like flotation reagents or machine oils), AuCarb™'s specific micro-porous dominance creates a steric hindrance against larger organic molecules, keeping the pores open for gold.
We strictly pack AuCarb™ in 25kg heavy-duty laminated elastic PE bags or 500kg bulk super sacks, ensuring the granules remain dry and uncrushed during global maritime transit.
AuLeach™ (GDA) is a revolutionary, eco-compliant chemical formulated to extract gold without the severe environmental toxicity of sodium cyanide. It provides comparable, and often superior, leaching kinetics.
Yes, AuLeach™ is certified globally as a Non-Hazardous general cargo. It bypasses toxic DG Class 6.1 legislation, meaning it requires no military escorts, reduces insurance premiums, and sails through customs smoothly.
AuLeach™ is designed as a direct drop-in substitute. Depending on the ore characteristics, it is typically dosed at a ratio of 1:1 to 1:1.5 compared to your historical sodium cyanide consumption.
No. The guaranteed operational pH range for AuLeach™ is 10.5 - 12. This aligns perfectly with traditional cyanidation circuits, meaning you can continue using standard hydrated lime to manage slurry alkalinity.
Zero equipment CAPEX is required. AuLeach™ is fully compatible with existing Heap Leaching irrigation networks, VAT leaching pools, and CIL/CIP mechanical agitators. No mechanical retrofitting is needed.
AuLeach™ exhibits superior resistance to interference from arsenic and sulfur. When treating complex refractory ores, it frequently achieves faster leaching kinetics and a 2% to 5% higher absolute recovery rate compared to traditional cyanide.
Absolutely. Because it lacks the persistent toxicity of cyanide, treating AuLeach™ tailings requires significantly fewer chemicals (like SO2/Air or Hydrogen Peroxide), slashing your environmental compliance and detox OPEX.
Mine laboratories can test AuLeach™ concentration via a standard chemical titration method using a silver nitrate complexing agent and a rhodanine indicator, exactly as your metallurgists currently do for cyanide.
Replacing toxic cyanide with AuLeach™ instantly elevates a mining company's ESG profile. It eliminates severe occupational health risks, protects local watersheds, and drastically improves relations with local communities and governments.
Yes, the gold complex formed by AuLeach™ is perfectly compatible with coconut shell activated carbon. Pairing it with AuCarb™ ensures a seamless transition in your CIL/CIP recovery and elution phases.
As a non-hazardous solid powder, AuLeach™ is efficiently packed in standard Net 25kg woven bags with inner moisture-proof liners, making it extremely easy to handle and mix at the plant.
High-clay laterites form extremely viscous slurries in CIL tanks, causing massive mechanical shear. You must use AuCarb™ AC60 (≥99% hardness) to prevent carbon from shattering into dust and losing your gold to the tailings.
Silver requires twice the cyanide to dissolve compared to gold. In high-silver ores (like those in Mexico), you must utilize ultra-pure AuCyan™ (≥98.3%) to provide an overwhelming surplus of CN⁻ ions, ensuring base metals don't exhaust your reagent.
Yes, but freezing temperatures severely retard chemical kinetics. In high-altitude regions (like the Andes or Central Asia), using the extreme purity of AuCyan™ helps jumpstart and maintain the dissolution equation despite poor thermodynamics.
AuLeach™ is highly effective in Vat leaching. Because it is non-toxic, it significantly reduces the environmental risk of pool leakage contaminating groundwater, making it ideal for artisanal and mid-scale operations.
Scaling is caused by high calcium and poor pH buffering. AuCyan™ contains strictly controlled Sodium Hydroxide (NaOH ≤0.13%), which stabilizes pH without triggering catastrophic calcium carbonate precipitation in your irrigation network.
For Carbon-in-Leach (CIL) and Carbon-in-Pulp (CIP), 8x16 mesh AuCarb™ is the industry standard. It provides a massive surface area for rapid adsorption while remaining large enough to be caught by standard inter-tank screens.
Desert operations often use saline water, which lowers dissolved oxygen and slows leaching. The explosive dissolution rate of high-purity AuCyan™ helps compensate for this lack of oxygen, maintaining acceptable extraction kinetics.
A cloudy pregnant solution often indicates high ash content or soft carbon degrading into fines. Switching to AuCarb™, with its ≤3% ash content and ≥99% hardness, ensures a pristine, clear liquor for electrowinning.
Transition sulfides consume immense oxygen and cyanide. Pre-aeration and lead nitrate conditioning are recommended. Following this, dosing AuCyan™ ensures sufficient active cyanide is available to overpower the remaining cyanicides.
Flotation reagents, machine oils, or humic acids from topsoil can blind carbon pores. AuCarb™’s highly specific microporous structure inherently resists large organic molecules, keeping the vital pores open for the gold complex.
Both work exceptionally well. However, if the tailings dam is near a local community or sensitive watershed, re-processing with AuLeach™ eliminates further toxic accumulation and simplifies final site rehabilitation.
We exclusively transact under strict FOB (Free On Board) China ports, or CIF (Cost, Insurance, and Freight) to your destination seaport globally.
No. Due to severe international safety regulations and the unpredictable nature of cross-border rail infrastructure, we strictly prohibit the use of international railway transport for hazardous chemical exports. We rely 100% on secure maritime freight.
For landlocked nations, we ship CIF to the nearest strategic coastal transit hub (e.g., Port of Arica for Bolivia, or Port of Dakar for Mali). From there, your designated local forwarder manages the cross-border road trucking.
In countries like Indonesia and the Philippines, domestic RORO ferries often refuse to carry toxic DG Class 6.1 cargo. Because AuLeach™ is Non-Hazardous, it can be seamlessly loaded onto any domestic ferry as general cargo.
A standard 1x20' FCL typically holds 20 Metric Tons (MT) of AuCyan™ when packed in 1,000kg wooden boxes, or approximately 18 to 21 MT when packed in 50kg steel drums, depending on precise pallet configurations.
Our UN-certified wooden boxes and steel drums feature integrated, thick Polyethylene (PE) inner liners that are heat-sealed. This creates a hermetic barrier, completely blocking extreme atmospheric humidity during Caribbean hurricanes or Asian monsoons.
Yes, all CIF shipments are covered by comprehensive marine insurance, protecting your chemical investment against the risks of trans-oceanic transit, rough seas, and port handling.
We handle the sea freight directly to your destination port. Once the containers are unloaded, the responsibility is passed cleanly to the buyer's localized logistics agents to manage customs clearance and inland trucking.
Yes, all wooden packaging utilized for AuCyan™ exports undergoes strict IPPC-certified fumigation and is stamped accordingly to comply with global agricultural and customs regulations.
We provide a complete suite of export documentation, including the Commercial Invoice, Packing List, Bill of Lading (B/L), Certificate of Origin (CO), and the comprehensive Material Safety Data Sheet (MSDS).
Due to stringent International Maritime Dangerous Goods (IMDG) codes regarding the segregation of hazardous and non-hazardous materials, AuCyan™ (Class 6.1) and AuCarb™ must be shipped in dedicated, separate containers.
If AuCyan™ mixes with water, it hydrolyzes. If it mixes with acids, it immediately releases highly toxic, lethal Hydrogen Cyanide (HCN) gas. It must be stored in a dry, strictly alkaline environment at all times.
Operators must wear full Personal Protective Equipment (PPE) including chemical-resistant gloves, full-face respirators equipped with specific cyanide gas cartridges, splash-proof goggles, and rubber boots.
Do not use water. Dry spills should be carefully swept up and placed into sealed containers. Any contaminated surfaces must be neutralized using a strong alkaline oxidizing solution (like sodium hypochlorite) while personnel wear full respirators.
Because AuLeach™ is non-hazardous and degrades naturally into non-toxic compounds, it requires minimal to zero specialized chemical detoxification before being discharged to the tailings dam, drastically reducing environmental liabilities.
Yes, our manufacturing facilities operate under strict ISO 9001 (Quality Management) and ISO 14001 (Environmental Management) certifications, ensuring global-grade consistency and safety.
Absolutely. Community protests often stem from the fear of toxic cyanide spills contaminating local water supplies. Implementing the non-toxic AuLeach™ physically eliminates this threat, serving as a powerful PR and community relations tool.
The INCO SO2/Air process is a common method to detoxify cyanide tailings. It utilizes sulfur dioxide and oxygen, catalyzed by copper, to oxidize toxic free cyanide into relatively harmless cyanate. (Note: Using AuLeach™ eliminates the need for this expensive process).
Storage facilities must be elevated, flood-proof, well-ventilated, and completely shielded from direct sunlight and rain. Acids and other reactive chemicals must be strictly quarantined in entirely separate buildings.
In case of inhalation or ingestion, move the victim to fresh air immediately and seek emergency medical attention. Cyanide antidote kits (such as Amyl Nitrite, Sodium Nitrite, and Sodium Thiosulfate) must be kept on-site and administered by trained professionals.
No. While basic dust masks should be worn during transfer, AuCarb™ is non-toxic and features an ultra-low attrition rate, minimizing the generation of airborne carbon dust in the plant environment.
Yes, the steel drums can be neutralized and recycled, and the robust wooden boxes can be repurposed safely on-site. The inner PE bags should be handled according to local hazardous waste protocols if they contained cyanide.
Precisely Match Your Gold Recovery Process with the Right Activated Carbon to Maximize Gold Recovery, Reduce Carbon Consumption, and Optimize Overall Operating Costs.
United Chemical’s newly developed premium gold recovery coconut shell activated carbon series (including BC1100, AuCarb™ AC50, AC55, and AC60) is engineered specifically for global metallurgical recovery networks. Our products deliver exceptional operational stability across diverse extraction frameworks, including aggressive Carbon-in-Pulp (CIP) and Carbon-in-Leach (CIL) circuits, high-volume Carbon-in-Column (CIC) loops, as well as complex Gold Ore Heap Leaching and continuous VAT Leaching / Tank Leaching facilities. Featuring outstanding mechanical hardness, an ultra-dense sub-nanometer microporous matrix, and highly optimized gold loading kinetics, our activated carbon effectively minimizes gold lock-up, limits carbon fines degradation, and drastically cuts soluble gold losses under the most rigorous, high-attrition mining environments worldwide.
Shaanxi United Chemical CO., Ltd. stands proudly as China's leading provider of gold mining chemicals and comprehensive engineering technology solutions. Our exceptional products and services have established a robust global footprint, covering over 77 countries and effectively supporting more than 200 major mining facilities worldwide.
To ensure long-term, superior performance when processing a wide variety of complex ores, we have specially engineered and developed the AuCarb™ series of premium, renewable granular microporous activated carbon. Exclusively tailored for highly efficient gold recovery processes (CIL & CIP), this series is strongly recommended for the initial filling of recovery circuits. It not only guarantees exceptional gold recovery rates but also significantly reduces activated carbon inventory losses.
To assist clients of varying production scales and ore grades in rapidly identifying the perfect fit, we have meticulously curated the following four core product lines: BC1100, AC50, AC55, and AC60.
Strategic Positioning: The ultimate cost-effective weapon for Heap Leaching and simplified CIP processes. Directly competing with and disrupting the conventional market, aiming to provide clients with the most highly competitive pricing through massive shipping volumes and economies of scale.
Applicable Scenarios: Heap Leach, simplified CIP workflows.
Target Clients: Entry-level/low-end application scenarios featuring lower production capacities, lower raw ore gold grades, and extremely strict cost-control requirements.
High Iodine Value Guarantee: Iodine number up to ≥1100 mg/g, ensuring robust foundational adsorption capabilities.
Wear-Resistant Design: Characterized by remarkably low platelet and attrition rates, with ball-pan hardness reaching ≥98.5%.
Physical Metrics: Apparent density tightly controlled at 0.40-0.50 g/ml, Total Ash Content ≤5%, Moisture ≤10%.
Selection Advice: Profit margins are entirely yielded to the customer, making it the perfect choice for projects demanding low procurement costs and massive bulk consumption.
Strategic Positioning: The premier choice for the vast majority of clients. Comprehensively benchmarking against the top-tier international brand Jacobi G208AS series, achieving the absolute perfect balance between supreme hardness, wear resistance, and adsorption kinetics.
Applicable Scenarios: Carbon-in-Pulp (CIP), Carbon-in-Leach (CIL), Carbon-in-Column (CIC).
Target Clients: Mid-tier users with moderate production capacities and relatively high gold grades.
Exceptional Mechanical Strength: Features ultra-low platelet content (≤5%) and ultra-low attrition (≤1.5%). Ball-pan hardness soars to ≥99%, drastically reducing tailing gold losses caused by mechanical wear.
Powerful Adsorption Kinetics: K-value reaches ≥26 Kg/t, R-value hits ≥50%, demonstrating outstanding adsorption capacity and velocity.
Physical Metrics: Apparent density 0.48-0.55 g/ml, Carbon Tetrachloride Activity (CTC) ≥50%.
Selection Advice: Delivering highly stable performance at a reasonable price point, it stands as the industry's golden standard for standard CIP/CIL/CIC circuits.
Strategic Positioning: SThe advanced upgrade for medium-to-large scale gold mines, Comprehensively benchmarking against the top-tier international brand Jacobi G209AS series, designed to further minimize carbon consumption while substantially elevating overall adsorption performance.
Applicable Scenarios: Carbon-in-Pulp (CIP), Carbon-in-Leach (CIL), Carbon-in-Column (CIC).
Target Clients: High-end users with large production capacities, high gold grades, and extreme sensitivity to material attrition and loss rates.
Enhanced Adsorption Performance: Adsorption capacity (K-value) elevated to ≥28 Kg/t, and adsorption rate (R-value) upgraded to ≥55%, significantly magnifying gold extraction efficiency.
Superb Wear Resistance: Maintains the excellent ≤5% platelet content and ≤2% ultra-low attrition , ensuring total granular integrity during prolonged, intense agitation.
Physical Metrics: Apparent density 0.45-0.55 g/ml, Carbon Tetrachloride Activity (CTC) increased to ≥55%.
Selection Advice: Notably reduces ton-ore carbon consumption, making it the ideal selection for large-scale chemical plants striving for the absolute optimization of comprehensive operational costs.
Strategic Positioning: The top-tier high-kinetic granular microporous carbon. Comprehensively benchmarking against Jacobi G210AS series. Engineered to maximize gold production yields and absolutely minimize carbon losses.
Applicable Scenarios: Carbon-in-Pulp (CIP), Carbon-in-Leach (CIL), Carbon-in-Column (CIC).
Target Clients: An exclusive group of cutting-edge clients (low in number but with the most stringent demands) operating with massive capacities, exceptionally high gold grades, and a relentless pursuit of ultimate recovery rates.
Unparalleled Adsorption Power: Boasts top-of-the-line adsorption capacity (K-value ≥30 Kg/t) and lightning-fast kinetics (R-value ≥60%).
Top-Tier Purity & Hardness: Total Ash Content ≤3%, Moisture ≤5%, Hardness ≥99%. Butane Activity up to ≥23%.
Process Optimization Guarantee: Its flawless 3D shape effectively prevents screen blinding. Low head loss tremendously optimizes adsorption kinetics, making it highly suitable even for the extraction of Glod-rich ores.
Selection Advice: Specifically designed for top-tier mining giants with a zero-tolerance policy for gold loss, brilliantly highlighting the brand's supreme technological prowess.
To facilitate a more intuitive selection process, we have summarized the core technical parameters of our four products.
*Based on standard 6x12 Mesh or 8x16 Mesh specifications; strictly packed in 25kg heavy-duty laminated elastic PE bags, We offer containerized global shipping under FOB, CIF, CFR terms.
*Execution Standards: Complies with American ASTM standards and A.A.R.L. internal mining testing standards. The product has passed third-party inspection and test samples can be provided.
| Core Testing Parameter | AuCarb™ BC1100 | AuCarb™ AC50 | AuCarb™ AC55 | AuCarb™ AC60 |
|---|---|---|---|---|
| Market Benchmarking Positioning | Conventional Heap Leach / High Cost-Performance | Comparable product: Jacobi G208AS | Advanced choice for Large Scale Comparable product: Jacobi G209AS | Comparable product: Jacobi G210AS |
| Apparent Density | 0.40 - 0.50 g/ml | 0.48 - 0.55 g/ml | 0.45 - 0.55 g/ml | 0.45 - 0.55 g/ml |
| Ball-pan Hardness | ≥ 98.5% | ≥ 99% | ≥ 99% | ≥ 99% |
| Platelet Content | ≤ 5% | ≤ 5% | ≤ 5% | ≤ 5% |
| Attrition | ≤ 2% | ≤ 1.5% | ≤ 2% | ≤ 2% |
| Total Ash Content | ≤ 5% | ≤ 3% | ≤ 3% | ≤ 3% |
| Moisture | ≤ 10% | ≤ 5% | ≤ 5% | ≤ 5% |
| Adsorption Capacity (K Value) | / | ≥ 26 Kg/t | ≥ 28 Kg/t | ≥ 30 Kg/t |
| Adsorption Rate (R Value) | / | ≥ 50% | ≥ 55% | ≥ 60% |
| Iodine Number | ≥ 1100 mg/g | / | / | / |
| Butane Activity | / | ≥ 19.5% | ≥ 21% | ≥ 23% |
| CTC (Carbon Tetrachloride Activity) | / | ≥ 50% | ≥ 55% | / |
As a premier provider of engineering technology solutions, AuCarb™ activated carbon perfectly aligns with the following typical design parameters of large-scale plants:
| Treatment Capacity | CIP Configuration(125000t per month) | CIL Configuration(250000t per month) |
|---|---|---|
| Gold Head Grade | 4 g/t | 4 g/t |
| Pulp FlowRate | 240 m³/h | 475 m³/h |
| No. of Contactors | 6 | 8 |
| Volume of Contactors | 160 m³ | 1780 m³ |
| Mass of AuCarb™ | 5 t per contactor | 20 t per contactor |
| Rate of AuCarb™ Transfer | 2.75 t per day | 5.5 t per day |
Whether you are operating a heap leaching project with a limited initial budget, or managing a massive CIL plant relentlessly pursuing the ultimate recovery of every single gram of gold, AuCarb™ provides the most perfectly tailored technical-grade activated carbon for you. Our particle size distribution is exceptionally uniform (particles larger than the upper mesh limit and smaller than the lower mesh limit are strictly controlled within < 5.0% and < 4.0% respectively), eliminating pipeline blockage and gold loss risks right from the source. Immediate contact us today!
| ShaanXi United Chemical Co., Ltd. Address: Jinhui Global Plaza, Qujiang District, Xi'an, Shaanxi Province, P.R. China Mobile / WhatsApp:+86 17392705576 | Email:info@unitedchemicalcn.com Website:www.unitedchemicalcn.com Focusing on Gold Mining & Precious Metal Extraction Solutions. Pioneer | Collaborate | Communicate | Dedicated | Honesty | Win-win |
Reaching the Leaching Ceiling: Precision Chemicals for Global Gold Mining Efficiency
In the modern gold mining landscape, the gap between standard recovery and peak efficiency is defined by reagent precision.
United Chemical, with 26+ years of frontline expertise serving 77 countries, presents the AuCyan™ NaCN Series—not just a chemical, but a meticulously engineered leaching engine.
Surpassing industry benchmarks, our latest production batches consistently achieve "Superior Quality" grades. Below is the certified performance data (Ref: Batch C050030HS251101).
| Testing Items | Standard (GB/T 19306-2003) | AuCyan™ (Typical) | Operational Impact |
|---|---|---|---|
| Sodium Cyanide (NaCN) | ≥ 98.0% | 98.3% | Maximum gold dissolution kinetics and recovery rates. |
| Sodium Hydroxide (NaOH) | ≤ 0.5% | 0.13% | Superior pH stability; prevents premature hydrolysis. |
| Sodium Carbonate (Na2CO3) | ≤ 0.5% | 0.18% | Minimized impurity interference in the leaching solution. |
| Moisture (H2O) | ≤ 0.9% | 0.3% | Enhanced solid stability during long-term storage and sea transit. |
| Insoluble Substances | ≤ 0.05% | 0.02% | Anti-clogging formula; protects critical pumps and nozzles. |
To a professional mine manager, these numbers are not just statistics—they are the key indicators of operational health and metallurgical certainty.
In Heap Leaching and CIL circuits, water-insoluble matter is the silent enemy. AuCyan™ reduces this to a negligible 0.02%, ensuring continuous operation with zero downtime for nozzle cleaning and extended equipment longevity by reducing abrasive wear on dosing pumps.
Maintaining a strict 0.13% NaOH level prevents the passivation of gold surfaces in specific ore types. AuCyan™ allows for precise pH modulation, ensuring the chemical environment is optimized solely for gold complexation rather than neutralizing excess alkaline impurities.
The 98.3% purity standard ensures a higher activity of CN⁻ ions. This triggers accelerated leaching kinetics, which is critical for processing refractory ores or maximizing throughput in high-capacity metallurgical plants.
United Chemical delivers the certainty of profit through vertical integration. AuCyan™ is engineered to work in molecular harmony with our ecosystem:
✔AuCarb™ Activated Carbon: High-purity leaching creates a "cleaner" pregnant solution, allowing our high-hardness coconut shell carbon to adsorb gold with maximum efficiency and minimal pore interference.
✔AuLeach™ Eco-Reagents: For mines with strict environmental mandates, our reagents provide a hybrid path to sustainability without sacrificing recovery benchmarks.
| Type of Packaging | Loading Capacity (20’FCL / 40’FCL) |
|---|---|
| 50kg Iron Drum (Standard) | 18 MT / 26 MT |
| 50kg Iron Drum (with Tray/Pallet) | 13.5 MT / 25 MT |
| 1000kg Wooden Box | 20 MT / 26 MT |
| 1100kg Wooden Box | 22 MT / 26.4 MT |
ISO 9001, ISO 22716, cGMP Certified
Kosher & Halal Certified
Full Compliance with International Cyanide Management Code
MOQ: Consult our sea trade manager for specific route details.
Loading Ports: Shanghai, Ningbo, Guangzhou, Qingdao, Tianjin, Dalian, Xiamen, Lianyungang.
Delivery Time: 4-6 weeks (destination dependent).
We don't just sell chemicals; we deliver a "Second Command Center" for your site. With expert resident teams in Africa, SE Asia, and Central Asia, we provide the metallurgical experience of 200+ mining companies.
Contact Our Technical Group TodayHigh Hardness & Rapid Adsorption Activated Carbon for CIL/CIP Gold Extraction
The "Profit Guardian" for Gold Recovery. Engineered for Maximum Adsorption, Zero-Waste Hardness, and Superior CIL/CIP Performance.
In modern gold recovery (CIP/CIL), while Sodium Cyanide determines how much gold is dissolved, Activated Carbon determines how much gold is actually kept. AuCarb AC50 is not just a filter medium; it is a high-performance catalyst for your mine's profitability.
Sourced from high-altitude, aged coconut shells in Southeast Asia and processed via advanced steam activation, it solves the critical pain points of "carbon loss, low loading, and attrition".
Data Formula: High Iodine Adsorption + Extreme Hardness = Zero Loss Recovery
| Particle Size (6x12 mesh) | 98.3% Distribution | Apparent Density | 0.48 - 0.55 g/cc |
| Moisture Content | ≤ 5% | Carbon Content | Pure Coconut Shell Base |
In high-agitation tanks, carbon collisions are violent. A 1% increase in attrition is not just lost carbon—it's gold-loaded carbon escaping into waste. AuCarb AC50 maintains peak structural integrity.
Our carbon achieves an R-Value (Adsorption Kinetics) ≥ 50%. This means gold ions are "locked" instantly, preventing losses even during surge flows or fluctuating ore grades.
Uniform particle size (6x12 mesh) and low platelet levels ensure your inter-stage screens never clog, maintaining smooth pulp flow and preventing mechanical downtime.
+0.1-0.3g
Extra Gold Recovered per Ton
-20%
Carbon Consumption Reduction
95%+
Activity Recovery after Reactivation
Contact our global technical team for a full COA report or on-site sampling.
We don't just sell chemical parameters; we deliver 5-10 years of operational certainty.
WhatsApp: +86 173 9270 5576
Multiple Names
Gold recovery activated carbon
Gold extraction activated carbon
Coconut shell activated carbon for gold recovery
Gold mining activated carbon
Activated carbon for gold extraction
Coconut activated carbon gold mining
Gold adsorption activated carbon
Gold processing activated carbon
Coconut shell charcoal for gold extraction
Premium gold recovery carbon
Active carbon for gold recovery
Activated charcoal for gold mining
Gold cyanide adsorption carbon
CIP activated carbon (Carbon-in-Pulp)
CIL activated carbon (Carbon-in-Leach)
CIC activated carbon (Carbon-in-Column)
Heap leaching activated carbon
Vat leaching activated carbon
Carbon in pulp gold recovery
Carbon in leach gold extraction
Gold cyanidation process carbon
Gold leaching carbon adsorption
Carbon desorption gold process
Elution circuit activated carbon
Gold elution carbon
Tailings gold recovery carbon
High hardness activated carbon gold
Attrition resistant carbon gold recovery
Gold activated carbon R value
Gold activated carbon K value
Ball-pan hardness activated carbon
Low platelet generation carbon gold
High gold loading capacity carbon
Microporous carbon for gold cyanide
Low ash activated carbon gold mining
Preg-robbing prevention activated carbon
Gold cyanide complex adsorption
Activated carbon iodine value gold mining
CTC activated carbon gold
6x12 mesh activated carbon gold
8x16 mesh activated carbon gold
6x16 mesh gold recovery carbon
12x30 mesh activated carbon gold
Granular activated carbon for gold
Irregular granular carbon gold mining
High density gold carbon
Gold carbon particle size distribution
Gold recovery activated carbon manufacturer
Coconut shell carbon supplier for gold mines
CIP activated carbon factory
Wholesale gold extraction carbon
Activated carbon price per ton gold mining
Bulk activated carbon for gold recovery
Gold mining chemicals supplier
CIL activated carbon exporter
Gold recovery carbon FOB price
Buy activated carbon for CIP plant
Premium coconut carbon manufacturer
Gold carbon 25kg bag / 500kg jumbo bag
Activated carbon regeneration gold plant
Thermal regeneration of carbon gold
Acid washing activated carbon gold
Carbon reactivation efficiency gold
Carbon attrition loss gold plant
Reducing soluble gold loss
Gold carbon fouling prevention
Carbon inventory management gold CIP
Carbon transfer rate CIL
Gold carbon stripping process
AuLeach™ Series: The Revolutionary Seamless Substitute for Sodium Cyanide, High-Recovery Green Mining Reagents: HS Code 3824999999
AuLeach™ GDA eco-friendly leaching agent, It Can Replace The Application Of NaCN Without Changing The Original Process, With Green Environmental Protection, Stable Indicators, Safe Use, Low Comprehensive Cost Advantages.
Revolutionizing gold extraction with seamless replacement for Sodium Cyanide. Engineered for Profit, Certified for Safety, and Built for a Green Mining Future.
As global environmental regulations tighten, the "hidden costs" of Sodium Cyanide—including specialized transport, armed escorts, complex permitting, and high tailings treatment expenses—can severely erode your project's profitability.
"AuLeach™ is not just a reagent; it is an industrial-strength solution designed to reach the theoretical ceiling of gold extraction without the regulatory burden. It offers seamless substitute, allowing mines to bypass the 'Red Tape' of cyanide management while maintaining premium recovery rates."
Designed for "Drop-in Replacement." You do not need to modify existing CIP, CIL, or Heap Leaching infrastructure. Maintain your standard pH (10.5–11.5) and alkalinity controls while simply switching the reagent.
Field data from 77 countries shows AuLeach™ can shorten adsorption equilibrium time by 2–4 hours. This increases plant throughput and optimizes the efficiency of our AuCarb™ Activated Carbon.
Classified as a common chemical, AuLeach™ eliminates the need for armed escorts, hazardous storage bunkers, and complex environmental discharge permits. It is a "Common Cargo" for sea and rail.
Adjust pH to 11 ± 1 using lime or caustic soda. Stable alkalinity ensures the complex organic compounds in AuLeach™ stay active and prevents passivation of the gold surface.
Typical dosage: 0.5 - 1.0 kg per Ton of ore. The high selectivity of AuLeach™ reduces interference from harmful substances like arsenic and sulfur, stabilizing the recovery curve.
Unit Packaging: 25 KG/Bag
Material: PE Paper-Plastic Composite with internal moisture-proof film.
Security: Tamper-proof and heavy-duty for rugged transit.
| Container Type | Max Net Weight |
|---|---|
| 20' FCL | 26,000 KG (26 MT) |
| 40' FCL | 28,000 KG (28 MT) |
Born in the heart of China’s gold industry, we provide more than just reagents. We deliver a technical synergy where AuLeach™ (Leaching), AuCyan™ (Booster), and AuCarb™ (Adsorption) work in molecular harmony to secure an extra 2%-5% recovery gain for your mine.
Flexible working time / commission / remote work / travel expenses included
We are seeking a dynamic individual based in Indonesia to fill the role of a Flexible Customer and Supplier Relations Specialist. This position offers the flexibility to work on an as-needed basis, aligning with our project timelines and deal flow. As part of our team, you will be responsible for managing communications with customers and suppliers, conducting product quality assessments, and overseeing the smooth progression of operations.
1. Maintain effective communication with customers and suppliers, responding to inquiries and feedback promptly.
2. Conduct on-site visits across various locations in Indonesia to assess product quality and ensure compliance with standards.
3. Collaborate with internal teams to coordinate logistics, monitor shipments, and address any operational challenges.
4. Prepare detailed reports on quality assessments, propose enhancements, and suggest improvements to optimize product quality.
5. Act as a liaison between the company, customers, and suppliers to facilitate communication and resolve issues as they arise.
- Proficiency in Bahasa Indonesia and English (additional regional languages preferred).
- Strong interpersonal skills and the ability to cultivate positive relationships.
- Experience in quality control, supply chain management, or related fields is advantageous.
- Willingness to travel within Indonesia and work independently.
- Excellent organizational skills and attention to detail.
This position offers a flexible work schedule, allowing you to engage when deals are active. If you are a proactive individual with a commitment to customer satisfaction and product quality, we encourage you to apply for this role. Join us in delivering exceptional service and products to our valued customers in Indonesia.
Please send your resume and a cover letter detailing your relevant experience and why you are interested in this position to [echo@unitedcc.net].
Flexible working time / commission / remote work / travel expenses included
Job Description:
We are seeking a dynamic individual based in Thailand to fill the role of a Flexible Customer and Supplier Relations Specialist. This position offers the flexibility to work on an as-needed basis, aligning with our project timelines and deal flow. As part of our team, you will be responsible for managing communications with customers and suppliers, conducting product quality assessments, and overseeing the smooth progression of operations.
Key Responsibilities:
1. Maintain effective communication with customers and suppliers, responding to inquiries and feedback promptly.
2. Conduct on-site visits across various locations in Thailand to assess product quality and ensure compliance with standards.
3. Collaborate with internal teams to coordinate logistics, monitor shipments, and address any operational challenges.
4. Prepare detailed reports on quality assessments, propose enhancements, and suggest improvements to optimize product quality.
5. Act as a liaison between the company, customers, and suppliers to facilitate communication and resolve issues as they arise.
Qualifications:
- Proficiency in Thai and English (additional regional languages preferred).
- Strong interpersonal skills and the ability to cultivate positive relationships.
- Experience in quality control, supply chain management, or related fields is advantageous.
- Willingness to travel within Thailand and work independently.
- Excellent organizational skills and attention to detail.
This position offers a flexible work schedule, allowing you to engage when deals are active. If you are a proactive individual with a commitment to customer satisfaction and product quality, we encourage you to apply for this role. Join us in delivering exceptional service and products to our valued customers in Thailand.
How to Apply:
Please send your resume and a cover letter detailing your relevant experience and why you are interested in this position to [ echo@unitedcc.net ].
Flexible working time / commission / remote work / travel expenses included
Job Description:
We are searching for a dynamic individual based in Laos to take on the role of a Flexible Customer and Supplier Relations Specialist. This position offers flexibility to work on a project basis, aligning with our flow and operational requirements. As a valuable member of our team, you will be responsible for managing communications with customers and suppliers, conducting product quality assessments, and ensuring seamless operations.
Key Responsibilities:
1. Maintain effective communication with customers and suppliers, promptly addressing inquiries and feedback.
2. Conduct on-site visits to various locations in Laos to evaluate product quality, ensure compliance with standards, and provide comprehensive reports.
3. Collaborate with internal teams to manage logistics, monitor shipments, and address operational challenges.
4. Prepare detailed quality assessment reports, propose enhancements, and recommend strategies to improve product quality.
5. Act as a key liaison between the company, customers, and suppliers to facilitate communication, resolve issues, and ensure smooth operations.
Qualifications:
- Proficiency in English is required, with knowledge of local Lao languages considered a plus.
- Strong interpersonal skills and the ability to establish positive relationships with customers and suppliers.
- Previous experience in quality control, supply chain management, or related fields is advantageous.
- Willingness to travel within Laos as needed and the ability to work autonomously.
- Exceptional attention to detail and a dedication to providing excellent service.
Additional Information:
This role offers a flexible work schedule, allowing you to engage when there are active projects. If you are a proactive individual committed to customer satisfaction and product quality, we encourage you to apply for this position. Join us in delivering outstanding service and products to our valued customers in Laos.
Job Title: Flexible Customer and Supplier Relations Specialist (Location - Myanmar)
ကျွန်တော်တို့ဟာ မြန်မာနိုင်ငံမှာ အခြေချထားတဲ့ လှုပ်ရှားမှုရှိတဲ့ ပုဂ္ဂိုလ်တစ်ယောက်ကို ရှာဖွေနေပါတယ်။ ဤအနေအထားက ကျွန်ုပ်တို့၏စီးဆင်းမှုနှင့် လုပ်ငန်းဆောင်တာလိုအပ်ချက်များနှင့် ကိုက်ညီစေသည့် စီမံကိန်းအခြေခံအားဖြင့် ပြောင်းသာလွှဲသာရှိစေသည်။ ကျွန်ုပ် တို့ အသင်း ၏ အဖိုးတန် အဖွဲ့ဝင် တစ် ဦး အနေဖြင့် ၊ သင် သည် ဖောက်သည် များ နှင့် ထောက်ပံ့ သူ များ နှင့် ဆက်သွယ်ရေး ကို စီမံ ခန့်ခွဲ ခြင်း ၊ ထုတ်ကုန် အရည်အသွေး အကဲဖြတ် မှု များ ကို ဆောင်ရွက် ခြင်း ၊ နှင့် ပိတ်ဆို့ မှု မ ရှိ သော လုပ်ငန်းစဉ် များ သေချာ စေရန် တာဝန် ရှိ လိမ့်မည် ။
We are looking for an active person based in Myanmar. This position allows flexibility on a project basis to meet our flow and operational needs. As a valuable member of our team, You manage communications with customers and suppliers. Conducting product quality evaluations; and will be responsible for ensuring that the process is free of bottlenecks.
အဓိကတာဝန်များ -
၁။ ဖောက်သည်တွေနဲ့ ထောက်ပံ့ပေးသူတွေနဲ့ ထိရောက်တဲ့ ဆက်သွယ်မှုကို ဆက်ထိန်းထားပါ။ စုံစမ်းမေးမြန်းမှုတွေနဲ့ တုံ့ပြန်မှုတွေကို ချက်ချင်းဖြေရှင်းပေးပါ။
. ကုန်ပစ္စည်းအရည်အသွေးကို အကဲဖြတ်ရန်၊ စံနှုန်းများကို လိုက်နာရန် သေချာစေရန်နှင့် ကျယ်ကျယ်ပြန့်ပြန့် အစီရင်ခံစာများပေးရန် မြန်မာနိုင်ငံရှိ နေရာအသီးသီးသို့ သွားရောက်လည်ပတ်ခြင်း။
၃။ ပြည်တွင်းအဖွဲ့တွေနဲ့ ပူးပေါင်းပြီး ကုန်ပစ္စည်းတွေကို စီမံခန့်ခွဲဖို့၊ ကုန်တင်ပို့မှုတွေကို စောင့်ကြည့်ဖို့နဲ့ လုပ်ငန်းစိန်ခေါ်ချက်တွေကို ကိုင်တွယ်ဖြေရှင်းဖို့ပါ။
၄။ အရည်အသွေးအသေးစိတ် အကဲဖြတ်မှတ်တမ်းများကိုပြင်ဆင်ပါ၊ တိုးမြှင့်ပေးရန် အဆိုပြုပြီး ထုတ်ကုန်အရည်အသွေး တိုးတက်စေရန် နည်းဗျူဟာများကို အကြံပြုပါ။
၅။ ကုမ္ပဏီ၊ ဖောက်သည်များနှင့် ထောက်ပံ့ပေးသူများစပ်ကြား အဓိကဆက်သွယ်မှုတစ်ခုအနေနှင့် အက်ဥပဒေအနေနှင့် ဆက်သွယ်ရေးလွယ်ကူစေရန်၊ ပြဿနာများကိုဖြေရှင်းရန်နှင့် ချောမွေ့သောလုပ်ငန်းများကို သေချာစေရန် ကုမ္ပဏီ၊ ဖောက်သည်များနှင့် ထောက်ပံ့ပေးသူများစပ်ကြား အဓိကဆက်သွယ်မှုတစ်ခုအဖြစ် လုပ်ဆောင်ပါ။
Key Responsibilities:
1. Maintain effective communication with customers and suppliers. Respond promptly to inquiries and responses.
. to evaluate product quality; Visiting various locations in Myanmar to ensure adherence to standards and provide comprehensive reports.
3. Collaborate with local teams to manage products; To monitor shipments and address business challenges.
4. Prepare detailed quality assessment records; Propose enhancements and suggest strategies to improve product quality.
5. the company, Act as a key link between customers and suppliers to facilitate communication; Company to resolve issues and ensure smooth operations. Act as a primary liaison between customers and suppliers.
အရည်အချင်းများ -
- အင်္ဂလိပ်ဘာသာစကားဖြင့် ကျွမ်းကျင်မှုလိုအပ်သည်။ ဒေသခံမြန်မာဘာသာစကားများ၏ အသိပညာဖြင့် ခိုင်မာသော အပြန်အလှန် ကျွမ်းကျင်မှုများနှင့် ဖောက်သည်များနှင့် ထောက်ပံ့ပေးသူများနှင့် အပြုသဘောဆောင်သော ဆက်ဆံရေးများ တည်ဆောက်နိုင်စွမ်းရှိသည်ဟု ယူဆကြသည်။
- အရည်အသွေးထိန်းချုပ်မှု၊ ထောက်ပံ့ရေးဆက်သွယ်ရေး စီမံခန့်ခွဲမှု ဒါမှမဟုတ် ဆက်စပ်နေတဲ့ လယ်ကွင်းတွေမှာ အရင်တွေ့ကြုံမှုက အကျိုးရှိပါတယ်။
- လိုအပ်သလို မြန်မာနိုင်ငံအတွင်းမှာ ခရီးသွားဖို့ တလိုတလားရှိခြင်းနဲ့ အလိုအလျောက် အလုပ်လုပ်နိုင်စွမ်း။
- အသေးစိတ်အချက်အလက်တွေကို အထူးဂရုစိုက်ပြီး ကောင်းမွန်တဲ့ ဝန်ဆောင်မှုတွေ ထောက်ပံ့ပေးဖို့ ဆက်ကပ်အပ်နှံမှု။
ဤအခန်းကဏ္ဍက ပြောင်းသာလဲသာရှိသော အလုပ်ဇယားတစ်ခုဖြစ်ပြီး တက်ကြွလှုပ်ရှားသော စီမံကိန်းများရှိသည့်အခါ စေ့စပ်စေသည်။ အကယ်၍ သင်သည် ဖောက်သည်များ ကျေနပ်မှုနှင့် ကုန်ပစ္စည်းအရည်အသွေးအတွက် ကတိပြုထားသော တက်ကြွလှုပ်ရှားသူတစ်ဦးဖြစ်မည်ဆိုလျှင် ဤရာထူးအတွက် လျှောက်လွှာတင်ရန် သင့်အားပေးပါသည်။ မြန်မာနိုင်ငံမှာ တန်ဖိုးရှိတဲ့ ဖောက်သည်တွေကို ထူးခြားတဲ့ ဝန်ဆောင်မှုနဲ့ ထုတ်ကုန်တွေ ပေးပို့ရာမှာ ကျွန်တော်တို့နဲ့ ပူးပေါင်းပါ။
Qualifications -
- Proficiency in the English language is required. Strong interpersonal skills with knowledge of local Burmese languages and the ability to build positive relationships with customers and suppliers are considered.
- Quality control; Prior experience in supply chain management or related field is beneficial.
- Willingness to travel within Myanmar as needed and ability to work independently.
- Attention to detail and dedication to providing excellent service.
This role has a flexible work schedule and is engaged when there are active projects. If you are an activist committed to customer satisfaction and product quality, we encourage you to apply for this position. Join us in delivering exceptional services and products to our valued customers in Myanmar.
Flexible working time / commission / remote work / travel expenses included
We are seeking a dynamic individual located in Nigeria to fill the position of a Flexible Customer and Supplier Relations Specialist. This role offers flexibility to work on a project-by-project basis, aligning with our deal flow and operational requirements. As a key member of our team, you will be responsible for managing communications with customers and suppliers, conducting product quality assessments, and ensuring the smooth running of operations.
Key Responsibilities:
1. Maintain effective and timely communication with customers and suppliers, addressing inquiries and feedback promptly.
2. Conduct on-site visits to various locations in Nigeria to assess product quality, verify compliance with standards, and provide detailed reports.
3. Collaborate with internal teams to coordinate logistics, monitor shipments, and troubleshoot operational challenges.
4. Prepare comprehensive reports on quality assessments, propose improvements, and recommend strategies to enhance product quality.
5. Serve as a liaison between the company, customers, and suppliers to facilitate communication, address any issues, and ensure seamless operations.
Qualifications:
- Fluent in English and knowledge of local Nigerian languages is an advantage.
- Strong interpersonal skills and the ability to build positive relationships with customers and suppliers.
- Previous experience in quality control, supply chain management, or related fields is beneficial.
- Willingness to travel within Nigeria as needed and the ability to work independently.
- Excellent organizational skills, attention to detail, and a commitment to delivering top-notch service.
This role provides a flexible work schedule, allowing you to engage when projects are active. If you are a proactive individual dedicated to customer satisfaction and product quality, we encourage you to apply for this opportunity. Join us in our mission to provide exceptional service and products to our customers in Nigeria.
Flexible working time / commission / remote work / travel expenses included
We are looking for a dynamic individual based in India to fill the role of a Flexible Customer and Supplier Relations Specialist. This position offers the flexibility to work on an as-needed basis, aligning with our project timelines and deal flow. As part of our team, you will be responsible for managing communications with customers and suppliers, conducting product quality assessments, and overseeing the smooth progression of operations.
Key Responsibilities:
1. Maintain effective communication with customers and suppliers, responding to inquiries and feedback promptly.
2. Conduct on-site visits across various locations in India to assess product quality and ensure compliance with standards.
3. Collaborate with internal teams to coordinate logistics, monitor shipments, and address any operational challenges.
4. Prepare detailed reports on quality assessments, propose enhancements, and suggest improvements to optimize product quality.
5. Act as a liaison between the company, customers, and suppliers to facilitate communication and resolve issues as they arise.
Qualifications:
- Proficiency in English and Hindi (additional regional languages preferred)
- Strong interpersonal skills and the ability to cultivate positive relationships- Experience in quality control, supply chain management, or related fields advantageous- Willingness to travel within India and work independently- Excellent organizational skills and attention to
This position offers a flexible work schedule, allowing you to engage when deals are active. If you are a proactive individual with a commitment to customer satisfaction and product quality, we encourage you to apply for this role. Join us in delivering exceptional service and products to our valued customers in India.